CNC Automatic Rebar Cage Forming & Welding Workstation
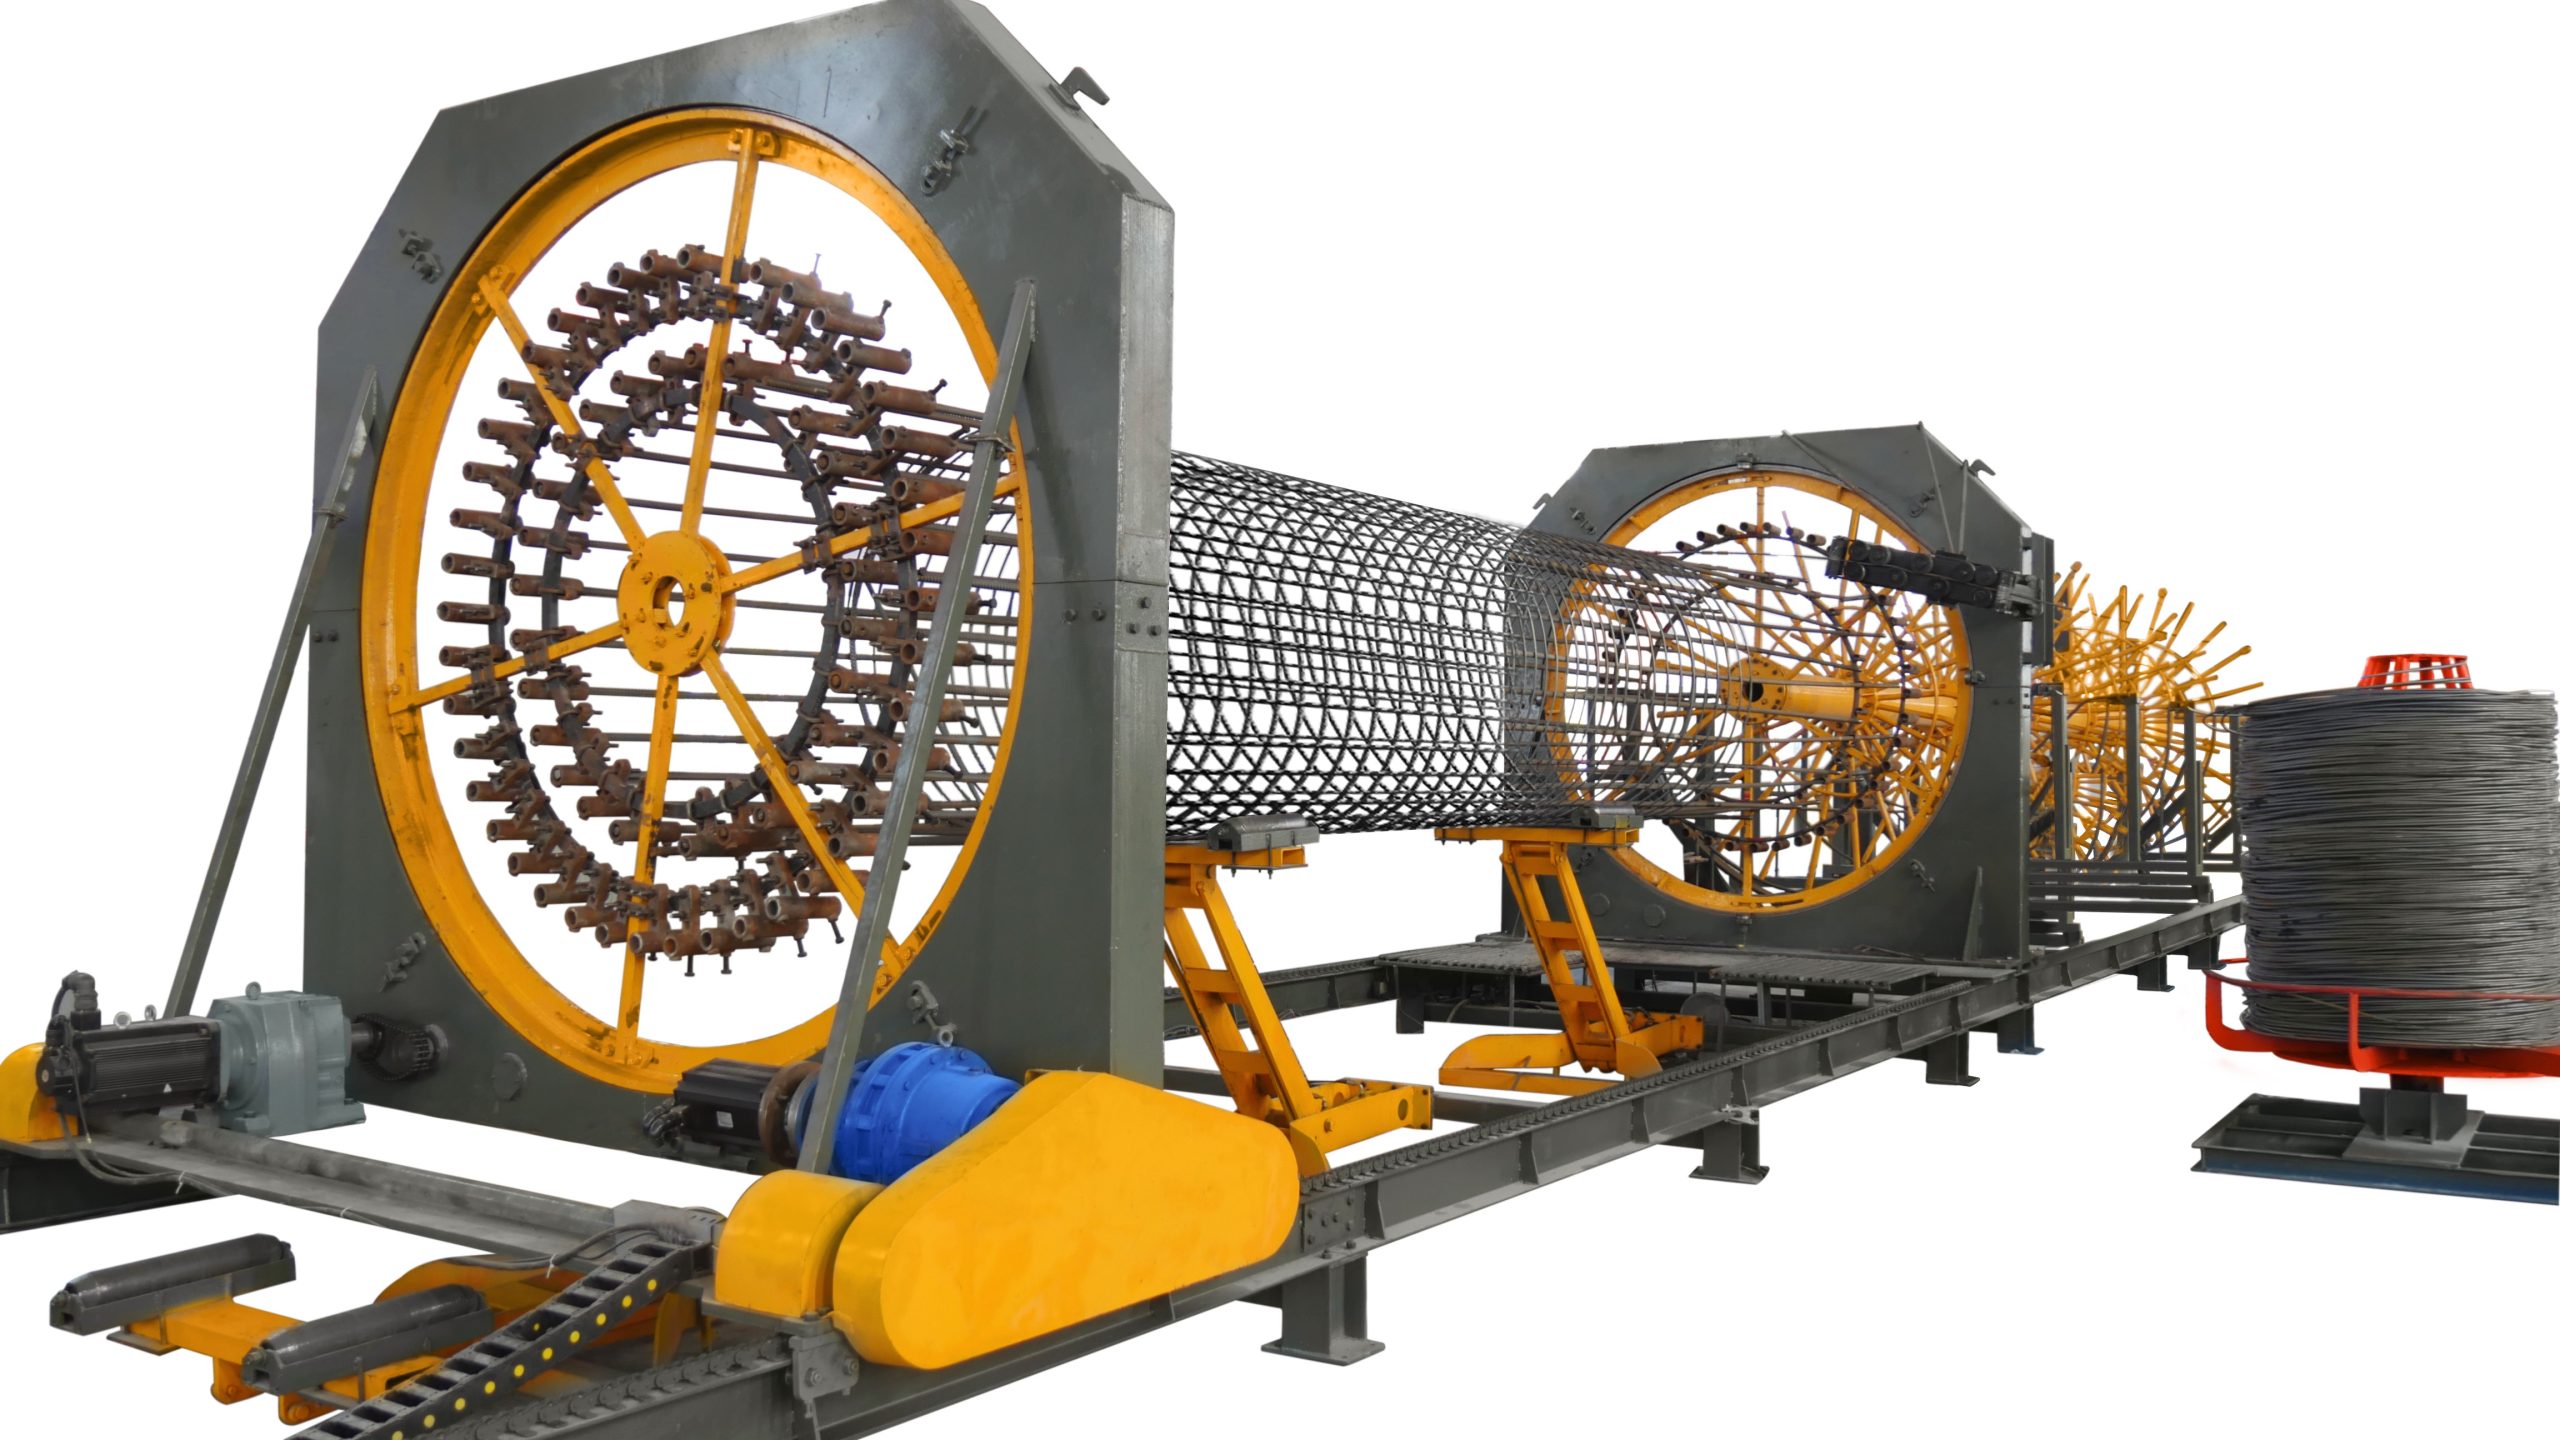
The CNC Automatic Rebar Cage Forming & Welding Workstation (HBZN-2200) is a complete automated line for pile foundation projects. It combines servo-positioned main bar feeding, a six-axis welding robot, and parallel frame and spiral winding stations to produce standard rebar cages from 800–2200 mm in diameter and 12 m in length. With only 1–2 operators, it can process more than 20 finished cages per day, with even bar spacing and about 1.5% steel saving compared with manual work.
Since 1996
Manufacturer in Changge City
20,000 m²
Factory, 150+ employees
ISO9001
SGS / TUV inspected, CE certified
24h online
Pre-sale and after-sale support
CNC Automatic Rebar Cage Forming & Welding Workstation Description
800–2200 mm
Cage inner diameter12 m
Cage length20+ / day
12 m cages, 2 operators≈1.5%
Steel saved vs. manual lappingPRODUCT OVERVIEW
Replace point-by-point manual welding with a repeatable, automated process
The Intelligent CNC Rebar Cage Forming & Welding Workstation automatically welds coiled spiral bars to main bars to produce standard pile foundation rebar cages.Manual cage fabrication depends on hand-marked spacing, experience-based spiral pitch and long labor time, which leads to inconsistent diameter and rework at supervision acceptance. This workstation combines automatic main bar feeding, servo positioning, six-axis robot welding and separate frame and spiral stations running in parallel.The HBZN-2200 is a redesign of our existing rebar cage welding workstation. Key structures have been optimized to significantly reduce manufacturing cost while keeping full processing capability.01
Fast processing
With 2 operators over two shifts, more than 20 finished 12 m cages per day, including all preparation and installation steps.02
Stable quality
CNC operation gives even main bar and spiral spacing and consistent cage diameter, reducing the burden of supervisor spot checks.03
Steel saving
Continuous winding and tightening without laps saves about 1.5% of material compared with manual work.04
Traceable quality
Process parameters are stored and managed by the CNC system for quality control records.EQUIPMENT COMPOSITION
Four major mechanisms, commissioned independently or run together
Mechanism 1
Automatic Feeding Mechanism
Automatic main bar feeding, online spacing adjustment, length detection and positioning. Pneumatic feeding with servo positioning; alignment accuracy 3 mm.Mechanism 2
Rebar Cage Frame Welding Mechanism
Positioning welding of main bars to internal stiffener rings to form the cage frame. 6 internal stiffener rings with spacing set by CNC program.Mechanism 3
Rebar Cage Spiral Winding Mechanism
Coil straightening and winding at the set pitch. Drum-type dual-line straightening with payout speed adjustable by frequency converter.Mechanism 4
Spiral Bar Automatic Welding Robot
A six-axis robot follows the spiral bar path and welds each intersection of spiral bar and main bar. Welding modes are selectable.Supporting systems: hydraulic lifting support system (4 sets), electric rebar cage supports, single-side cage unloading device, and a CNC operating system (touch screen + PLC).CORE ADVANTAGES
Built to remove the slow, inconsistent steps of manual cage making
01
Automatic feeding, online spacing adjustment
Main bar spacing is adjusted online with low positioning error. Length detection holds the main bar end position within 2 mm and spacing within 10 mm.02
Six-axis robot automatic welding
Spiral bar and main bar intersections are welded automatically with no manual involvement, directly saving welder positions.03
Suits multiple cage types
Welds single main bar with single stirrup, single main bar with double stirrups, and double main bars with double stirrups.04
Servo fixed-spacing structure
A servo system positions the main bars for even circumferential distribution and small error.05
Automatic ring-expanding device
Internal stiffener rings are easy to install. The expanding action is program-controlled, with action time set on the parameter page.06
Single-side cage unloading
Hydraulic supports lower, the door opens and the finished cage comes off the machine, shortening auxiliary time per cage cycle.07
Parallel frame and spiral stations
Frame welding and spiral bar welding proceed separately without waiting for each other, multiplying overall line efficiency compared with single-station rolling welders.08
Automated CNC system
Touch-screen operation stores up to 20 sets of rebar cage process data with an intelligent rebar length memory. Recall data when changing specifications, with no re-calibration of tool setting.09
Standardized finished cages
Consistent diameter and evenly distributed main bars make positioning easy when joining cage sections, saving on-site lifting and joining time.TECHNICAL PARAMETERS
HBZN-2200 specifications
| Parameter | Value |
|---|---|
| Model | HBZN-2200 |
| Rebar cage inner diameter | 800–2200 mm |
| Rebar cage length | 12 m |
| Maximum rebar cage weight | 6,000 kg |
| Complete machine weight | 25 t |
| Overall dimensions (L × W × H) | 35 m × 8 m × 3 m |
| Power supply | 380 V / 50 Hz |
| Rated total power | 85 kW (including 8 welding machines) |
| Number of operators | 1–2 persons |
| Parameter | Value |
|---|---|
| Main bar diameter | 16–32 mm |
| Spiral bar (coil) diameter | 8–14 mm |
| Spiral bar pitch | 70–300 mm |
| Spiral bar type | Single winding / double winding |
| Main bar type | Single main bar / double main bars |
| Main bar welding passes | 0–3 passes |
| Spiral bar welding mode | Full weld / staggered (quincunx) weld / self-adjusting |
| Single-point welding time, spiral bar | 0–1 s per point |
| Spiral bar welding speed | 0–16 m/min, servo adjustable |
| Parameter | Value |
|---|---|
| Machine head travel speed | 0–3 m/min |
| Spiral winding carriage speed | 1 m/min (design speed) |
| Cage rotation speed | 0–10 r/min |
| Spiral bar payout speed | 0–50 m/min, frequency converter adjustable |
| Spiral bar straightening | Drum-type dual-line straightening |
| Main bar feeding | Pneumatic automatic feeding |
| Rebar alignment | Servo positioning |
| Rebar alignment accuracy | 3 mm |
| Spiral bar spacing accuracy | ±2 mm |
| Cage rotation accuracy | ±0.2° |
| Main bar end position control | ≤ 2 mm |
| Main bar spacing control | ≤ 10 mm |
| Parameter | Value |
|---|---|
| Hydraulic station / oil pump pressure | 10 MPa |
| Air pump pressure | 0.8 MPa |
| Cage lifting | Hydraulic system, 4 support sets |
| Cage support | Electric support |
| Cage unloading | Single-side door |
| Cage diameter adjustment | Motor-driven linkage, 800–2200 mm, no molds required |
| Stored process data sets | Up to 20 sets, with intelligent rebar length memory |
| Internal stiffener rings per cage | 6 |
| Stiffener ring spacing range | 1500–2000 mm, set by CNC program |
| Spiral winding load capacity | 6,000 kg |
| Roller spacing adjustment | 500–1,400 mm |
| Control system | Touch screen + PLC |
| Parameter | Value |
|---|---|
| Model | HBZN-2200 |
| Rebar cage inner diameter | 800–2200 mm |
| Rebar cage length | 12 m |
| Maximum rebar cage weight | 6,000 kg |
| Complete machine weight | 25 t |
| Overall dimensions (L × W × H) | 35 m × 8 m × 3 m |
| Power supply | 380 V / 50 Hz |
| Rated total power | 85 kW (including 8 welding machines) |
| Number of operators | 1–2 persons |
| Parameter | Value |
|---|---|
| Main bar diameter | 16–32 mm |
| Spiral bar (coil) diameter | 8–14 mm |
| Spiral bar pitch | 70–300 mm |
| Spiral bar type | Single winding / double winding |
| Main bar type | Single main bar / double main bars |
| Main bar welding passes | 0–3 passes |
| Spiral bar welding mode | Full weld / staggered (quincunx) weld / self-adjusting |
| Single-point welding time, spiral bar | 0–1 s per point |
| Spiral bar welding speed | 0–16 m/min, servo adjustable |
| Parameter | Value |
|---|---|
| Machine head travel speed | 0–3 m/min |
| Spiral winding carriage speed | 1 m/min (design speed) |
| Cage rotation speed | 0–10 r/min |
| Spiral bar payout speed | 0–50 m/min, frequency converter adjustable |
| Spiral bar straightening | Drum-type dual-line straightening |
| Main bar feeding | Pneumatic automatic feeding |
| Rebar alignment | Servo positioning |
| Rebar alignment accuracy | 3 mm |
| Spiral bar spacing accuracy | ±2 mm |
| Cage rotation accuracy | ±0.2° |
| Main bar end position control | ≤ 2 mm |
| Main bar spacing control | ≤ 10 mm |
| Parameter | Value |
|---|---|
| Hydraulic station / oil pump pressure | 10 MPa |
| Air pump pressure | 0.8 MPa |
| Cage lifting | Hydraulic system, 4 support sets |
| Cage support | Electric support |
| Cage unloading | Single-side door |
| Cage diameter adjustment | Motor-driven linkage, 800–2200 mm, no molds required |
| Stored process data sets | Up to 20 sets, with intelligent rebar length memory |
| Internal stiffener rings per cage | 6 |
| Stiffener ring spacing range | 1500–2000 mm, set by CNC program |
| Spiral winding load capacity | 6,000 kg |
| Roller spacing adjustment | 500–1,400 mm |
| Control system | Touch screen + PLC |
Specifications are for the standard model and may be adjusted for customized configurations. Contact us to confirm parameters for your project.
WORKING PROCESS
From specification to finished cage in six steps
No manual involvement is needed in any welding step of the whole process.
STEP 1
Recall specification
On the touch screen, recall stored process data (up to 20 sets) or create a new specification.STEP 2
Automatic main bar feeding
Pneumatic feeding places main bars at the set quantity and spacing; servo positioning aligns them and length detection confirms end positions.STEP 3
Internal stiffener ring installation
Place the inner ring on its support and press install; the support expands and positions it automatically.STEP 4
Frame welding
The welding head travels along the cage body and welds each main bar to the internal stiffener rings to form the cage frame.STEP 5
Spiral winding and welding
Coil is straightened by the drum-type dual-line straightener and wound at the set pitch while the six-axis robot welds the intersections.STEP 6
Cage discharge
Hydraulic supports lower, the door device opens and the finished cage comes off the machine.CONTROL SYSTEM
Touch screen + PLC CNC system
- Store, recall and modify up to 20 rebar cage specification sets
- Main bar setup wizard guides the feeding parameters
- Action delay of each actuator can be set independently
- Automatic alarm when a position sensor times out without reaching position
- Independent start / stop / pause / reset control of main bar operation
 3D layout: main bar feeding station, frame welding head, spiral winding mechanism and cage discharge device.
APPLICATION FIELDS
Centralized prefabrication of pile foundation rebar cages
Especially suited to batch production for bored cast-in-place piles and large-diameter pile foundation projects.01
Metro
Station and tunnel foundation piles02
Bridges
Large-diameter bored pile cages03
Buildings
High-rise pile foundations04
Airports
Runway and terminal foundation works05
Expressways
Viaduct and bridge piling06
Foundation Engineering
Batch production for bored cast-in-place pilesApplicable practice: stiffener ring spacing
Pile cage design notes commonly call for reinforcing rings every 2 m, and every 1.5 m when the pile length exceeds 20 m. The HBZN-2200 sets ring spacing from 1500 to 2000 mm by CNC program. Always follow your project drawings and local codes.FAQ
Frequently asked questions about the HBZN-2200
What is a rebar cage welding workstation used for?
It is automated equipment for prefabricating pile foundation rebar cages. It feeds main bars, winds spiral bars around them and welds the intersections automatically, producing standard cages for bored cast-in-place piles and large-diameter pile foundations in metro, bridge, building, airport and expressway projects.What cage diameter and length can the HBZN-2200 handle?
The HBZN-2200 produces rebar cages with an inner diameter of 800–2200 mm and a length of 12 m. Cage diameter is adjusted by a motor-driven linkage mechanism, so no molds are needed to change size within this range.How long does it take to produce one 12 m rebar cage?
Cycle time depends on cage diameter and reinforcement configuration. With the standard configuration and two operators over two shifts, the workstation can process more than 20 finished 12 m cages per day, including material preparation, welding, stiffener ring, inspection tube and guide spacer installation. Contact us for cycle times for your specific cage.How many operators does the machine need?
Only 1–2 operators are needed. Main bar feeding, frame welding, spiral winding and spiral-to-main-bar welding are all completed automatically, with limited manual assistance.Can it weld double main bars and double spiral bars?
Yes. It handles three pile foundation reinforcement configurations: single main bar with single stirrup, single main bar with double stirrups, and double main bars with double stirrups.What power supply and floor space are required?
The machine runs on 380 V / 50 Hz with a rated total power of 85 kW, including 8 welding machines. The overall dimensions are 35 m × 8 m × 3 m and the complete machine weighs about 25 t.Do you provide overseas installation and training?
Please contact our sales team to discuss installation, commissioning, operator training and remote technical support for your project and destination.Related Products
How We Work With You
- 1Solution Development
- 2Manufacturing and commissioning
- 3Operational Production
- 4Business Negotiation
Questions before you decide? See the FAQ.